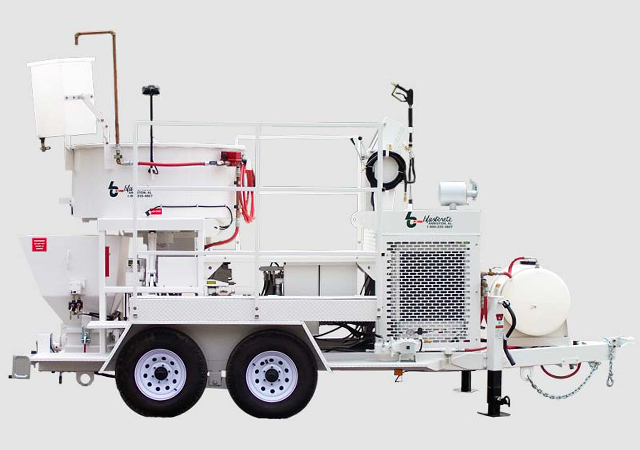
Looking for a reliable heavy duty mixer pump for demanding industrial refractory projects? The Blastcrete MX-10 Mixer/Pump is a high-performance mixing and pumping system designed for dense refractory shotcrete and pump-cast applications. Combining a high-torque hydraulic pan mixer with a 3-inch ultra-high-pressure swing tube piston pump, the MX-10 provides an integrated solution for mixing and delivering refractory materials in challenging industrial environments.
Since 1996, the MX-10 has been an established choice for monolithic refractory installations. With a specified pumping pressure of 2,200 PSI and a stated material delivery capacity of up to 10 tons per hour, this heavy-duty machine is designed to support demanding material placement operations.
The MX-10 is also commonly used to pump suitable refractory materials over vertical distances exceeding 300 feet, depending on material properties, pipeline configuration, and operating conditions. Its swing-out receiving hopper provides convenient access to the lower hopper and swing tube section for cleaning and maintenance.
Request a Quote or Download the Brochure to discover how the Blastcrete MX-10 can support your industrial mixing and pumping requirements.
What Is the Blastcrete MX-10 Heavy Duty Mixer Pump?
The Blastcrete MX-10 is a specialized mixer and pump engineered for dense refractory shotcrete and pump-cast installations. It combines material mixing and high-pressure pumping into one machine, helping contractors prepare and deliver suitable refractory materials for demanding industrial projects.
The system features a 2,200-pound-capacity high-torque hydraulic pan mixer and a 3-inch × 24-inch ultra-high-pressure swing tube piston pump. This combination supports material preparation and delivery for monolithic refractory installations where reliable performance and consistent mixing are important.
For industrial contractors searching for a heavy duty mixer pump, the MX-10 offers an integrated configuration designed to handle demanding refractory applications while providing practical access for cleaning and maintenance.
Key Features of the MX-10 Heavy Duty Mixer Pump
1. Ultra-High-Pressure Piston Pump
The MX-10 features a 3-inch × 24-inch ultra-high-pressure swing tube piston pump with a specified pumping pressure of 2,200 PSI.
This high-pressure pumping system is designed for dense refractory shotcrete and pump-cast applications where material must be delivered through a suitable pumping line.
Its configuration supports demanding industrial installation work involving compatible refractory materials and extended pumping distances.
2. High-Torque Hydraulic Pan Mixer
The MX-10 incorporates a hydraulic pan mixer with a capacity of 2,200 pounds.
The mixer has a stated mixing time of approximately 1.5 to 2 minutes, helping prepare suitable refractory materials for pumping and placement.
Proper mixing is essential for achieving the material consistency required by the selected installation method. Operators should follow the refractory manufacturer's mixing instructions and material specifications.
3. High Material Delivery Capacity
The MX-10 is designed to deliver up to 10 tons of refractory material per hour under suitable operating conditions.
Its technical specifications also list a volumetric output range of 0–12 cubic yards per hour. Actual production depends on material density, mix formulation, pipeline configuration, and job-site conditions.
This capacity makes the machine worth considering for industrial projects that require substantial refractory material placement.
4. Vertical Pumping Capability
The MX-10 is commonly used to pump suitable refractory materials over vertical distances exceeding 300 feet.
This capability can support installations where materials must reach elevated or difficult-to-access locations in industrial facilities.
Actual pumping distance depends on material properties, pipeline diameter and layout, elevation changes, and operating conditions.
5. Swing-Out Receiving Hopper
The machine features a swing-out receiving hopper with a stated capacity of 2,500 pounds and a hydraulic agitator.
The swing-out design provides access to the lower hopper and swing tube section for cleaning and maintenance. Forklift tubing mounted to the lower hopper also facilitates flat-pack removal.
These features help simplify equipment servicing and handling when performed according to the manufacturer's
Heavy Duty Mixer Pump Blastcrete MX-10 for Industrial Refractory Applications