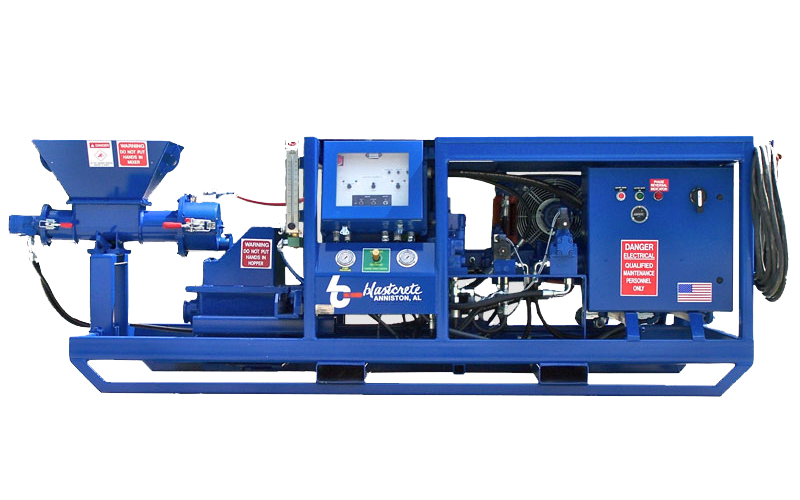
Choosing the right heavy duty concrete pumping system is essential for contractors who need reliable material delivery, consistent pumping performance, and efficient operation in demanding construction environments. Underground mining projects often present challenges such as restricted headroom, difficult access, long pumping distances, and limited availability of ready-mix concrete. The Blastcrete MineMate is designed to help address these challenges with an integrated concrete mixing and pumping solution.
The Blastcrete MineMate combines an X-10 ultra-high-pressure swing tube piston pump with a high-shear continuous mixer and a material screw conveyor. Designed for underground mine seals, grouting, and shotcrete applications, this machine supports projects where ready-mix concrete is not a practical option.
With a specified pumping pressure of 2,200 PSI, an output capacity of up to 12 cubic yards per hour, and the ability to pump material in excess of 500 feet, the MineMate is worth considering for suitable underground mining and construction applications.
What Is a Heavy Duty Concrete Pumping System?
A heavy duty concrete pumping system is designed to transport compatible concrete and cementitious materials to designated placement areas under demanding operating conditions. These systems are particularly valuable when materials must travel through extended delivery lines or reach locations that are difficult to access using conventional methods.
In underground mining, contractors may need specialized equipment that combines material preparation and pumping while operating in confined spaces. A suitable pumping system can help streamline material handling and support more efficient placement.
The Blastcrete MineMate integrates continuous mixing, material feeding, and high-pressure pumping into one low-profile machine designed for underground applications.
Introducing the Blastcrete MineMate
The Blastcrete MineMate is a specialized concrete mixing and pumping machine developed for underground mining and construction projects.
Its integrated design includes three main components:
X-10 ultra-high-pressure swing tube piston pump: Designed to pump compatible materials at high pressure.
High-shear continuous mixer: Prepares material for pumping.
Material screw conveyor: Feeds material into the continuous mixer and includes a bin indicator.
Combining these components helps coordinate material feeding, mixing, and delivery. This arrangement can be particularly useful on projects where transporting ready-mix concrete or positioning multiple machines is difficult.
Key Features of the Blastcrete MineMate
1. Ultra-High-Pressure Swing Tube Piston Pump
The MineMate features a 3-inch × 24-inch X-10 ultra-high-pressure swing tube piston pump.
The specified pumping pressure is 2,200 PSI, with an output range of 0–12 cubic yards per hour. These specifications make the machine worth evaluating for suitable high-pressure underground pumping applications.
Actual pumping performance depends on material consistency, aggregate characteristics, pipeline configuration, elevation changes, and operating conditions.
2. High-Shear Continuous Mixer
The integrated high-shear continuous mixer prepares material for pumping. Continuous mixing can help contractors coordinate material preparation with placement requirements, particularly when ready-mix concrete is unavailable or impractical.
For reliable operation, the selected mix design must be compatible with the pump, mixer, and delivery system.
3. Integrated Material Screw Conveyor
The MineMate includes a screw conveyor that charges the continuous mixer. A bin indicator helps operators monitor the material charging process.
This integrated feeding system supports an organized workflow between material supply, mixing, and pumping.
4. Low-Profile Design for Underground Projects
Limited overhead clearance is a common challenge in mining operations. The MineMate is designed to operate within a 6-foot ceiling, making it worth considering for suitable underground environments with restricted headroom.
The listed machine dimensions are 120 × 60 × 48 inches. Contractors should verify access routes, transport clearances, and available operating space before deployment.
5. Extended Pumping Distance
According to the manufacturer, the MineMate can pump material in excess of 500 feet.
This capability can help contractors evaluate the machine for underground projects where the placement location is far from the pumping equipment. Actual achievable distance depends on material properties, hose or pipeline diameter, routing, elevation, and job-site conditions.
6. Flexible Power Options
The Blastcrete MineMate offers two listed power configurations:
50 HP electric motor with starter and disconnect.
66 HP Kubota V3600 water-cooled diesel engine.
These options allow contractors to assess the equipment according to site power availability and operating requirements.
Underground applications must also account for applicable electrical safety standards, mine ventilation, diesel emissions controls, and operating regulations.
Technical Specifications of the Blastcrete MineMate
When comparing a heavy duty concrete pumping system, reviewing its technical specifications helps determine whether it meets project requirements.
Specification Details
Pump model X-10 ultra-high-pressure swing tube piston pump
Pump dimensions 3 inches × 24 inches
Pumping pressure 2,200 PSI
Output capacity 0–12 cubic yards per hour
Discharge 3-inch heavy-duty
Hopper capacity 3 cubic feet
Machine dimensions 120 × 60 × 48 inches
Machine weight 3,500 lbs.
Mixer type High-shear continuous mixer
Material feeding Screw conveyor with bin indicator
Operating clearance Designed for a 6-foot ceiling
Pumping distance In excess of 500 feet, according to the manufacturer
Electric power option 50 HP
Diesel power option 66 HP Kubota V3600
Confirm the final specifications, configuration, and material compatibility with the manufacturer before purchasing or deploying the equipment.
Benefits of a Heavy Duty Concrete Pumping System
Improved Material Handling
An integrated system combines material feeding, continuous mixing, and pumping in one machine. This can simplify coordination between material preparation and placement operations.
Reduced Dependence on Ready-Mix Delivery
The MineMate is designed for applications where ready-mix concrete is not a practical option. Its continuous mixing system supports on-site preparation of compatible materials for underground use.
Support for Long-Distance Pumping
The stated pumping capability beyond 500 feet makes the MineMate worth evaluating for underground projects where the placement area is located
Heavy Duty Concrete Pumping System: Discover the Blastcrete MineMate